
Hangbo Alloy Group
Shanghai · Est. 2012
Precision-wound MIG/TIG filler wire and coiled wire rod in Inconel, Hastelloy, Monel, and Incoloy grades. Diameter 0.8–5.0 mm. AWS ERNi classification with consistent arc performance.
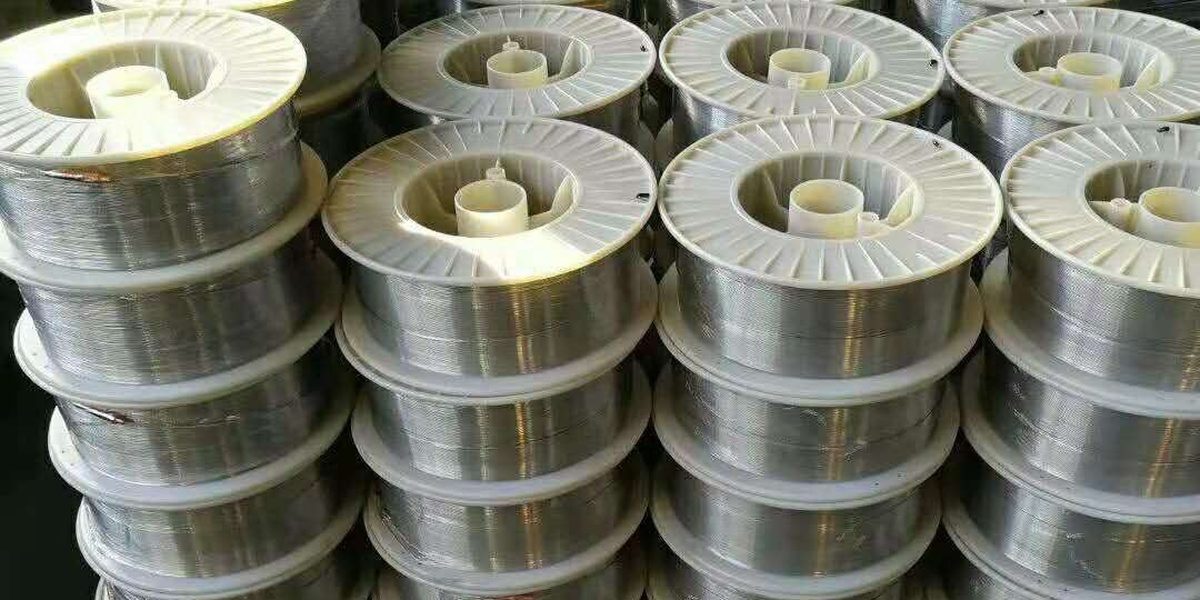
Hangbo Alloy Group manufactures nickel alloy welding wire with strict chemistry control and surface cleanliness. Our wire is produced from vacuum-melted ingots, drawn to precise diameters, and precision-wound onto spools or coils to ensure smooth, consistent feeding through welding equipment. The wire surface is cleaned and degreased to remove drawing lubricants that could cause porosity in the weld.
We supply welding wire for all major nickel alloy grades, matching filler metals to base metal compositions per AWS specifications. Each spool is labeled with wire classification, heat number, diameter, and net weight for full traceability.
| Parameter | Specification |
|---|---|
| Wire Diameter | 0.8 mm – 5.0 mm (TIG: 1.0–5.0mm; MIG: 0.8–2.4mm) |
| Diameter Tolerance | ±0.015 mm (under 1.6mm); ±0.025 mm (1.6–5.0mm) |
| Spool Sizes | D200 (5 kg) / D300 (15 kg) / D350 (20 kg) |
| Coil Weight | 5 kg – 300 kg |
| Cut Length (TIG) | 1,000 mm straight length (standard) |
| Surface Finish | Bright / Copper-coated / Chemically cleaned |
| Cast and Helix | Controlled for smooth MIG feeding (cast 200-500mm) |
| Winding Type | Precision layer-wound / Random wound |
| Packaging | Vacuum-sealed bag + desiccant + carton/drum |
| MOQ | 50 kg (standard); 200 kg (custom diameter) |
| Lead Time | 10–20 days (stock); 25–40 days (production) |
AWS A5.14 classified filler metals. Matching base metal shown for reference.
| AWS Class | Common Name | Ni | Cr | Mo | Fe | Nb+Ta | Ti | Other |
|---|---|---|---|---|---|---|---|---|
| ERNiCrMo-3 | Inconel 625 | 58 min | 20-23 | 8-10 | 5 max | 3.15-4.15 | 0.4 max | Al 0.4 max |
| ERNiCr-3 | Inconel 82 | 67 min | 18-22 | — | 3 max | 2-3 | 0.75 max | Si 0.5, Mn 2.5-3.5 |
| ERNiCrFe-7 | Inconel 52 | bal | 28-31.5 | 0.5 max | 7-11 | — | 0.5 max | Al 0.3-1.1 |
| ERNiCu-7 | Monel 60 | 62-69 | — | — | 2.5 max | — | 1.5-3.0 | Cu rem, Mn 4 max |
| ERNiCrMo-4 | Hastelloy C-276 | bal | 14.5-16.5 | 15-17 | 4-7 | — | — | W 3-4.5 |
| ERNiCrMo-10 | Hastelloy C-22 | bal | 20-22.5 | 12.5-14.5 | 2-6 | — | — | W 2.5-3.5 |
| ERNiMo-7 | Hastelloy B-2 | bal | 1.0 max | 26-30 | 2 max | — | — | C 0.02 max |
Vacuum induction melting for precise chemistry control
Multi-pass wet drawing with tight diameter tolerance
Chemical pickling and ultrasonic degreasing for porosity-free welds
Precision layer-wound spools for tangle-free MIG feeding
Spectrometry, diameter gauge, cast/helix test, surface inspection
Vacuum-sealed with desiccant to prevent oxidation in transit
| Standard | Scope |
|---|---|
| AWS A5.14 | Nickel and nickel alloy bare welding electrodes and rods |
| AWS A5.11 | Nickel and nickel alloy covered electrodes (SMAW) |
| ASME SFA-5.14 | ASME code case for nickel bare filler metal |
| ISO 18274 | International standard for nickel alloy welding consumables |
| EN ISO 18274 | European classification of nickel filler metals |
| AMS 5837 | Inconel 625 welding wire (ERNiCrMo-3) |
| AMS 5832 | Inconel 82 welding wire (ERNiCr-3) |
| NACE MR0175 | Sour service welding qualification requirements |
| ASME IX | Welding procedure and performance qualification |
The general rule is to match the filler metal composition to the base metal. For dissimilar metal joints (e.g., nickel alloy to steel), ERNiCr-3 (Inconel 82) is the most versatile choice. For weld overlay/cladding, ERNiCrMo-3 (Inconel 625) or ERNiCrMo-4 (Hastelloy C-276) provides excellent corrosion resistance. Our technical team can provide specific recommendations based on your application.
MIG wire (GMAW) is supplied on spools in continuous lengths, typically 0.8-2.4 mm diameter, and fed automatically through a welding gun. TIG wire (GTAW) is supplied in straight cut lengths (usually 1,000 mm) and manually fed into the weld pool. TIG wire diameters range from 1.0-5.0 mm. Both use the same AWS classification but differ in packaging form.
Yes. All our welding wire is manufactured to AWS A5.14 specifications. Each batch is tested for chemical composition, mechanical properties of deposited weld metal, and radiographic soundness. AWS classification, heat number, and test results are documented on the Certificate of Conformance supplied with each shipment.
Nickel alloy welding wire should be stored in its original vacuum-sealed packaging in a clean, dry environment at ambient temperature. Once opened, the wire should be used within 30 days or re-sealed in a moisture-free container. Do not store wire near acids, chlorine sources, or high-humidity areas. Pre-use cleaning is generally not required if packaging integrity is maintained.
Send us your AWS classification, diameter, spool size, and quantity. We respond within 10 minutes during business hours.